


Tapered Cork Stoppers, Cut to Your Bottle Neck — Not to a Stock Size
Product use: Agglomerated tapered stoppers for spirits, wine, olive oil, vinegar and small-batch food jars.
Starting requirement: Send a neck drawing, or one empty bottle.
Order requirement: No purchase order needed to start.
Sizing method: We size the top diameter from your neck ID and the compression you want, then cut a sample you can fit on the line.
Range and tolerance statement: Nothing here is “any size available”: these are the ranges and tolerances we hold, and they are why we turn down some drawings.
Top diameter range: Top Ø 18–26 mm.
Minimum order quantity: MOQ 1,000 pcs.
Sample lead time: Samples in 3–7 days.
Tolerance: Tolerance ±0.5 mm.
Description
Technical Parameters
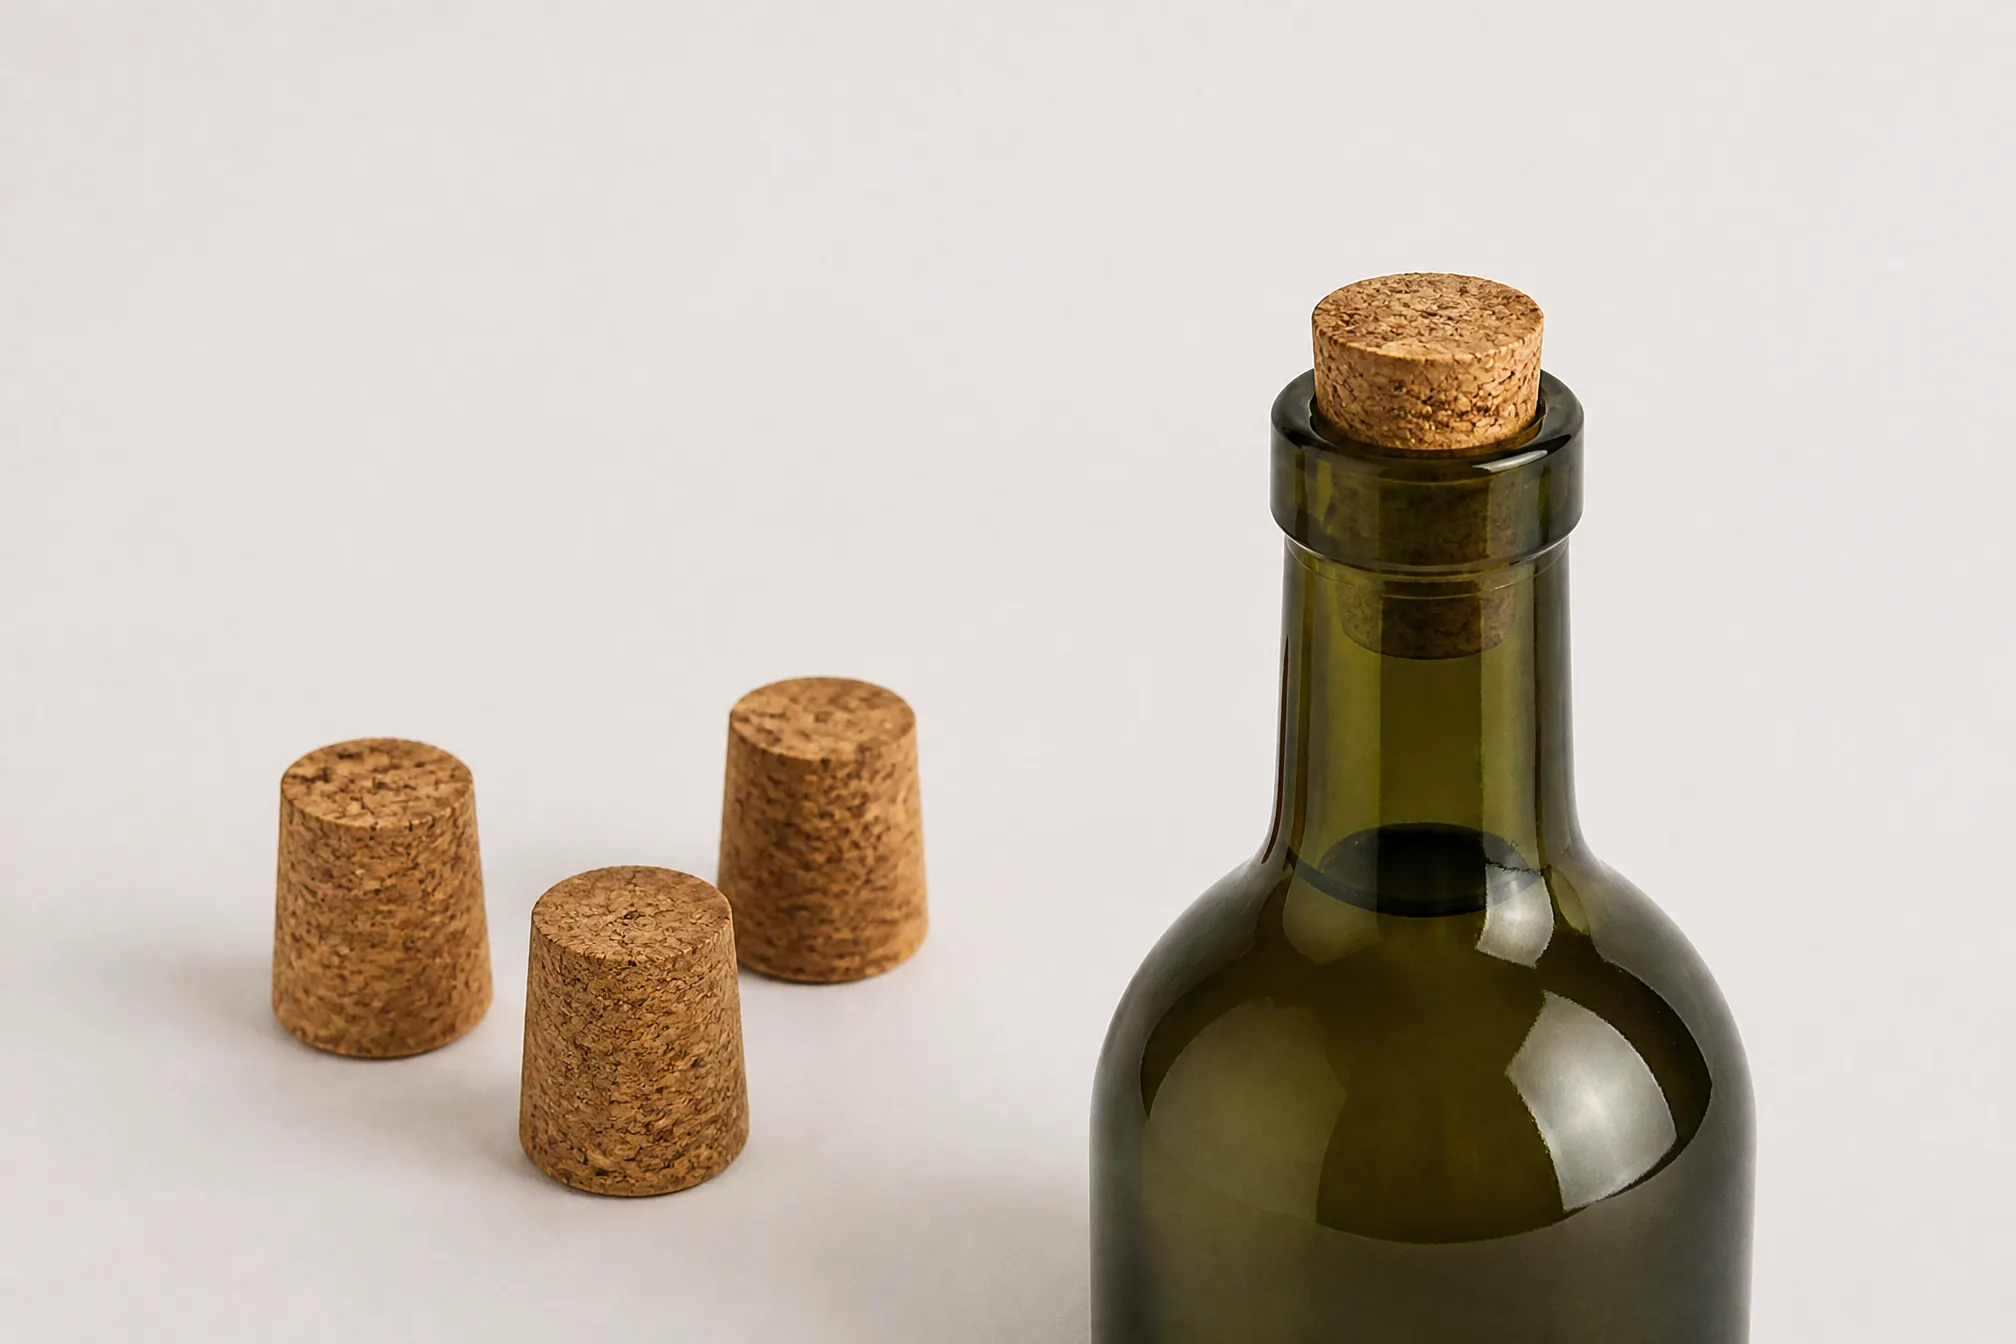
Six numbers that decide whether we can quote you
| Material | Agglomerated cork granules, food-grade binder |
| Top Ø / tolerance | 18–26 mm / ±0.5 mm |
| Length / tolerance | 20–45 mm / ±0.5 mm |
| Moisture | ≤ 8 % |
| MOQ | 1,000 pcs standard · 5,000 pcs full custom |
| Sample / bulk | 3–7 days / 20 days after drawing approval |
| Logo |
Laser engraving · hot stamping · pad printing |
Technical Specifications
| Material | Agglomerated cork granules, food-grade binder |
| Top diameter | 18–26 mm, in 0.5 mm steps |
| Bottom diameter | 15–23 mm |
| Length | 20–45 mm |
| Diameter tolerance | ±0.5 mm |
| Length tolerance | ±0.5 mm |
| Moisture content | ≤ 8 % |
| Taper | 1.5°–5.0° per side; fixed by your neck bore - see the constraint below |
| Surface | Natural · waxed · colour-stained |
| Logo method | Laser engraving · hot stamping · pad printing |
| MOQ | 1,000 pcs standard · 5,000 pcs full custom |
| Sample lead time | 3–7 days |
| Bulk lead time | 20 days after drawing approval |
| Payment | T/T 30 % deposit; sample freight deductible against the first order |
| Food contact | FDA 21 CFR 175.300 · EU 1935/2004 (declaration of conformity on request) |
| Wood sourcing | FSC® C167358 |
Why the tolerance rows matter more than the size rows. A stopper 0.5 mm under and one 0.5 mm over are both "in spec" and both called Ø24. In an 18.5 mm neck they produce 25.9% and 31.4% compression - one drops in, the other needs a mallet. A supplier who quotes a diameter without a tolerance has told you nothing you can check.

Which stopper for which neck
Measure the neck at the top edge, on the inside - not mid-bore, not the outside. Bore is tapered on most moulded bottles, and the top edge is what seals.
| Your neck ID | Our top Ø | Resulting compression | Note |
|---|---|---|---|
| 18.5 mm (standard wine) | 23.5–24.0 mm | 27–30% | Long body, 38–44 mm |
| 19.5 mm | 24.5–25.0 mm | 26–28% | Short body, 30–38 mm |
| 21.5 mm (spirits) | 26.0–26.5 mm | 21–23% | Short body, 26–32 mm |
| 25.0 mm (food jar) | 26.0–26.4 mm | 4–6% | Lid-style fit, no compression set |
| 13.0 mm (oils, samples) | 15.2–15.6 mm | 17–20% | Check dropper clearance |
| Other | Send a drawing or one bottle - we confirm the sizing before sampling, at no charge. | ||
The arithmetic, so you can check it yourself: compression % = (cork top Ø − neck ID) ÷ neck ID. An 18.5 mm neck with a 23.8 mm stopper gives (23.8 − 18.5) ÷ 18.5 = 28.6%. A caliper on the stopper and a bore gauge on the neck verify any row in two minutes.
The constraint nobody prints: top Ø, bottom Ø and length cannot all be free
The three ranges above are independent only on paper. In a physical stopper they are tied together by the taper, and the taper has to match your bottle's bore:
| Formula | half-angle θ = atan( ((top Ø − bottom Ø) ÷ 2) ÷ length ) |
| Worked example | Ø24 → Ø18 over 40 mm: atan(3 ÷ 40) = 4.29° per side. Change the length to 44 mm without touching the diameters and it becomes 3.90°, a 0.39° drift. You can't see it on paper. You can feel it in the neck. |
| Combination to avoid | Ø26 → Ø15 over 20 mm = 15.4° per side. That is a plug. It won't enter a moulded neck without distorting the bore. |
| What we hold | 1.5°–5.0° per side. Tell us your neck's bore angle and we cut to it; if you change the length, we re-derive the diameters instead of copying them. |
The five neck IDs in the table above are common industry sizes, not measurements of your bottle. Your drawing governs - the row is there so you can see the method, not to replace your caliper.

Four materials - and what each one costs you
| Type | Best for | Cost | What to know |
|---|---|---|---|
| Natural cork, whole bark, punched | Premium wine, visible top surface | €€€€ | Best-looking end grain, but grading is by eye - budget 5–8% cosmetic rejects. Longest lead time of the four. |
| Agglomerated cork granules + binder what we run most orders on |
Spirits, oils, vinegars, jars, private label | €€ | Dimensionally repeatable - this is why we can hold ±0.5 mm. The trade-off: it is not "100% natural cork", and we do not call it that. |
| Composite: cork body + wood or plastic cap | Spirits with a decorative head | €€€ | Two materials, two failure points. The joint is where a pull-test failure shows up first. |
| Synthetic TPR | High-speed lines, resealable spirits | €€ | Consistent to ±0.1 mm, but no cork texture - buyers notice. Not compostable. |
We do not sell whole-bark stoppers as agglomerated, or the reverse. If your spec sheet says 100% natural cork and your target price is our agglomerated price, one of the two has to change - usually the wording.

Logo methods, including where each one fails
Laser engraving
Burns the surface. No ink, no colour, matte dark line on natural cork. Minimum line width 0.3 mm.
The groove holds dust between its walls. On a light stopper, a serif logo under 0.4 mm fills in and reads as a smudge. Send vector art at final size, not a screenshot.
01
Hot stamping
Gold, silver or colour foil on the flat end. Crisp edges, reads as premium.
Foil sits on the surface and wears at the rim with handling - on a bottle opened nightly, expect visible wear within a season. Hairlines under 0.3 mm break during transfer.
02
Pad printing
1–3 spot colours, no gradients, sharp small text. Cheapest way to get a coloured logo.
Ink sits on a porous surface: it wears faster than foil under abrasion and is not alcohol-resistant at the contact edge. Not suitable for end-grain faces.
03
Unmarked
Lowest cost, cleanest look for brands using a neck capsule or a swing tag instead.
No brand presence once the capsule comes off - which is exactly the moment the guest picks it up.
04
Six things that go wrong with tapered stoppers
"It passed our filler. It still leaked."
1. The bottle passes inspection, then leaks in the warehouse
Bottle one looks right. The filler passes it, the capper passes it, the case ships. Twenty days later the carton has a ring on it.
Two mechanisms, and neither is visible at the filling head. First, insufficient radial compression for that batch of glass: moulded necks vary between cavities, and a stopper sized to the nominal drawing sits loose in the widest one. Second, moisture. A stopper compressed into a neck has to rebound against the bore wall. Wet cork rebounds slowly, so it seals late, after the case is already stacked.
We size from a measured neck ID, not the nominal on the drawing, and we hold moisture at or below 8 %.
How to check us: ask for the neck ID we sized against and the compression it produces. Then measure ten bottles from your own pallet - if our number sits inside the spread you find, the sizing was done on real glass.
"There was powder at the bottom of the bag."
2. The bottom of the bag
Open the poly bag and the bottom is pale. That powder is cork, and it goes into the bottle with the stopper.
Cutting a taper makes dust at the end face. A dull edge makes more, and a wide granule grading makes more again, because coarse grains tear instead of shearing. Nobody notices at the fill head. The customer notices in the bottle.
What controls it is the state of the cutting edge and whether the end face is cleaned after cutting - not the granule size on the datasheet. A cutter that is past its life cuts a ragged end face, and a ragged end face is where the dust comes from.
How to check us: take 200 pcs, tumble them in the bag for ten minutes, photograph the bag interior. Ten minutes, no lab, and it tells you more than any incoming inspection report.
"The first order was fine."
3. The reorder does not match the first order
The first order fitted. The reorder doesn't. The first guess is the binder. Ours was too. It wasn't the binder.
It was the cutting tool. A profile wears as it runs, and a worn tool cuts at the small end of the band while a fresh tool cuts at the large end. Both batches pass ±0.5 mm, and both feel different in the neck.
So pass/fail against a tolerance band is the wrong question. Ask for the measured mean per batch. Two batches can both be "OK" and still sit 0.3 mm apart at the mean.
How to check us: ask any supplier - including us - for the measured means of two consecutive batches of the same SKU. If the means drift, you will see it before your customer does. A supplier who only sends a pass certificate has not answered.
"Both are Ø24. They behave differently."
4. Five and a half points.
That is the spread ±0.5 mm produces in an 18.5 mm neck: 25.9 % at the low end, 31.4 % at the high end.
Two stoppers from the same carton. Both compliant. They behave like two products. This number decides whether your line runs at speed or an operator keeps a mallet at the station. It is also why we print tolerance instead of a nominal size alone - and why a quote that only says "Ø24" cannot be compared with ours.
How to check us: take ten stoppers at random, measure all ten, compute compression at the widest and the narrowest. That spread is the honest answer about any supplier, including us.
"Sometimes they're tight, sometimes loose."
5. You are comparing two batches, not two stoppers
Yes - and it is arithmetic, not luck. Two tolerances stack: the glass neck (about ±0.15 mm between cavities, more between moulds) and the cork (±0.5 mm). At the extremes the sum roughly doubles the nominal clearance.
That is why the neck ID you give us matters more than any other number on this page. The same Ø24 stopper is comfortable in a 19.0 mm neck and tight in an 18.4 mm one, and both necks can come off the same pallet.
How to check us: send ten bottles from the same pallet. We send back the ten measurements and the stopper size we would cut for the tightest of them.
"Our launch date is fixed."
6. The filling line does not wait for a container.
Which is why our lead time runs from drawing approval, not from inquiry, and why the production slot is held on payment rather than on a promise.
Twenty days after approval is our standard. The two things that move it are a profile that has to be cut from scratch, and orders confirmed after the seasonal window has filled. We would rather give you a date and keep it than take the order and slip.
How to check us: ask which line your SKU runs on and what that line's output at your size is. A supplier who answers with a plant-wide monthly figure is quoting the factory, not your order.
Where these go, with the sizes we ship
Spirits and craft distilling - short body, 26–32 mm long, Ø21.5–26.5 mm top, often foil-stamped. Or T-shape with a decorative head.
Wine and fruit wine - long body, 38–44 mm, Ø23.5–24.0 mm top, laser or unmarked under capsule. The 18.5 mm neck row above.
Olive oil and vinegar - 24–30 mm body, food-contact binder, no foil (the oil attacks the edge). Check the pourer clearance.
Essential oils and samples - Ø13–16 mm necks, 18–24 mm long. Check dropper clearance before choosing length.
Food jars: jam, honey, spice - lid-style fit at 4–6 % compression, 20–26 mm top Ø, waxed surface for moisture. Seals without a compression set.

From drawing to first sample, in 3 + 3–7 days
You send a drawing or one bottle - a photo with a caliper reading across the neck is enough to start.
We confirm the sizing - 3 days. You get the top Ø we recommend, the compression it produces, and the reason.
Sample is cut - 3–7 days. Sample free, freight at your cost, deductible against the first order.
Approval and payment - T/T 30 % deposit. The production slot is held on receipt.
Bulk run - 20 days after approval.
Packaging specification, HS code and certificate copies are issued with the quotation for your order - they differ by destination and by carton configuration.
The plant behind the page
22,000 m² in Xi'an, Shaanxi, 15 production lines, established 2007, exporting to more than 40 countries. Cork stoppers, lids and coasters run on separate lines from the yoga and flooring products, which is why a stopper order is scheduled by line and not by plant.
2007Established
22,000 m²Plant
15Production lines
40+Countries
ISO 9001Quality system

What buyers ask before the first sample
I have the neck ID. What top diameter do you cut?
Top Ø = neck ID × (1 + target compression). For an 18.5 mm neck at 28 % that is 23.7 mm, so we quote Ø23.5–24.0 mm with ±0.5 mm. Five common necks are worked out in the table above; send yours and we add the row.
My drawing says 24 mm with no tolerance. What now?
We ask which direction matters. If the filler jams, size to the low end of your glass; if it leaks, size up. A nominal diameter without a tolerance cannot be quoted precisely - it is the most common gap in incoming specs.
Does the stopper need to sit flush with the neck?
Only if a capsule or a label covers it. Otherwise leave 3–5 mm proud: it gives the customer something to grip, and it hides bore variation between cavities.
Is this natural cork or agglomerated?
Agglomerated - cork granules pressed with a food-grade binder. That is what allows a repeatable ±0.5 mm. Whole-bark natural stoppers exist and look different on the end grain; we will tell you which one your spec actually describes.
Which food-contact rules apply?
FDA 21 CFR 175.300 for the United States, and EU 1935/2004 with a declaration of conformity for the EU. Cork stoppers are not within the scope of the CE marking directives, so we do not claim CE - if your spec sheet asks for it, the food-contact documents are what you actually need.
Will an agglomerated stopper affect a high-proof spirit?
For long contact with 40 % ABV or above, a composite or synthetic closure is the safer specification, and it costs more. We would rather say that before quoting than sell you a cork that flavours the batch. For short contact, or anything below about 25 % ABV, agglomerated is the right choice.
What is the MOQ?
1,000 pcs for standard sizes off existing tooling; 5,000 pcs when a new profile has to be cut. Both figures are for one size and one finish.
How long is a sample, and how long is bulk?
3–7 days for the sample once the size is agreed; 20 days for bulk after approval and payment. They are quoted separately because they run on different equipment.
What if my launch date is already fixed?
Say so in the first message. Orders are scheduled against the slot held at payment, and a fixed date changes the sequence - sizing and sampling move to the front of the queue. It does not change the 20 days, and we will tell you if the date is not reachable instead of taking the order.
How do I know the second order will match the first?
Ask for the measured mean of each batch, not a pass certificate. Two batches can both sit inside ±0.5 mm and still be 0.3 mm apart at the mean - that is what your operator feels. Retained samples from earlier batches are the other half of the answer: ask to see one alongside the current run.
Hot Tags: Tapered Cork Stoppers, Cut to Your Bottle Neck — Not to a Stock Size, China Tapered Cork Stoppers, Cut to Your Bottle Neck — Not to a Stock Size manufacturers, suppliers, factory, Natural Cork Stopper Bottle, Natural Cork Material, Glass Bottle With Cork Lid, Small Glass Bottles With Cork Stopper, Small Glass Jar With Cork, Cork Lid Natural
Previous
Synthetic Wine Cork StpopperNext
cork bottle stopperSend Inquiry


